ISO 9001:2015
Quality management. Sets how every job is planned, checked and corrected, from enquiry through to despatch.
Scope Covers
Manufacture of grey iron and ductile (SG) iron castings.
Technocast Foundry is an ISO 9001, ISO 14001, ISO 45001, IATF 16949 and PED certified foundry in Coimbatore, Tamil Nadu, India. Every casting passes eight control points between raw material and the packing bay, checked in our own metallurgical lab, on two Brown and Sharpe coordinate measuring machines, and by in-house ultrasonic and magnetic particle testing.
How quality is built here
Process defines
the product.
Certifications
Five management systems, all current and independently audited by TÜV. The certified scope is the manufacture of grey iron and ductile (SG) iron castings. Every certificate can be downloaded further down this page.
ISO 9001:2015
Quality management. Sets how every job is planned, checked and corrected, from enquiry through to despatch.
Scope Covers
Manufacture of grey iron and ductile (SG) iron castings.
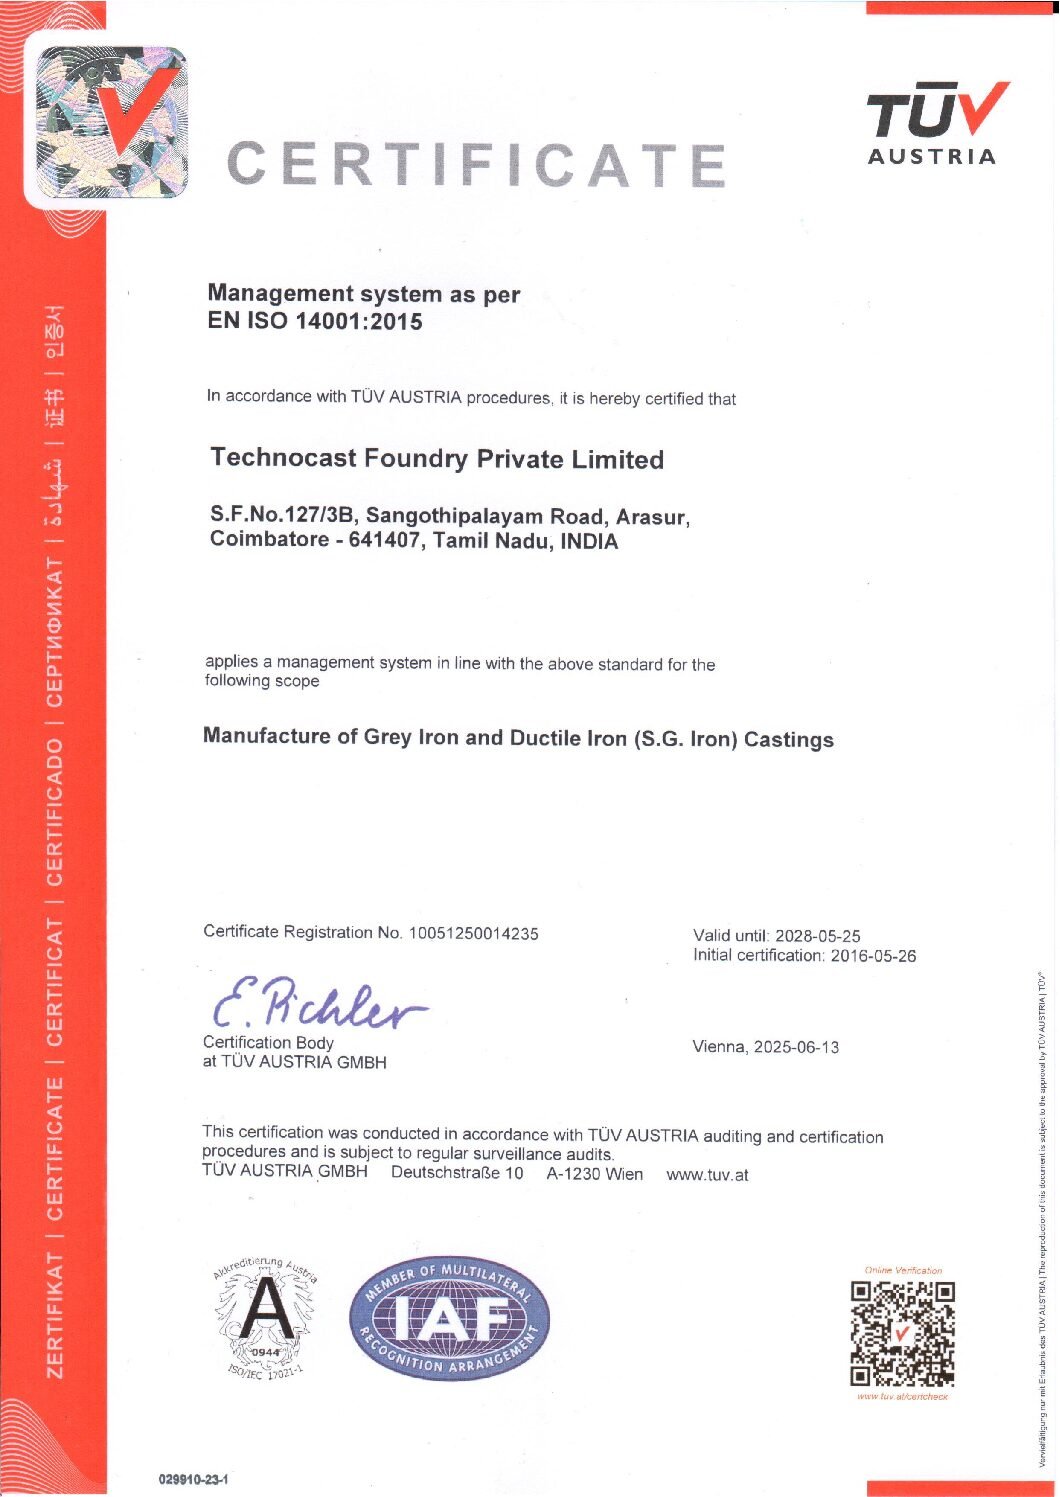
ISO 14001:2015
Environmental management. Covers how the plant manages emissions, effluent, waste and energy use. TÜV AUSTRIA certificate 10051250014235, certified since May 2016 and valid to 25 May 2028.
Scope Covers
Manufacture of grey iron and ductile (SG) iron castings.
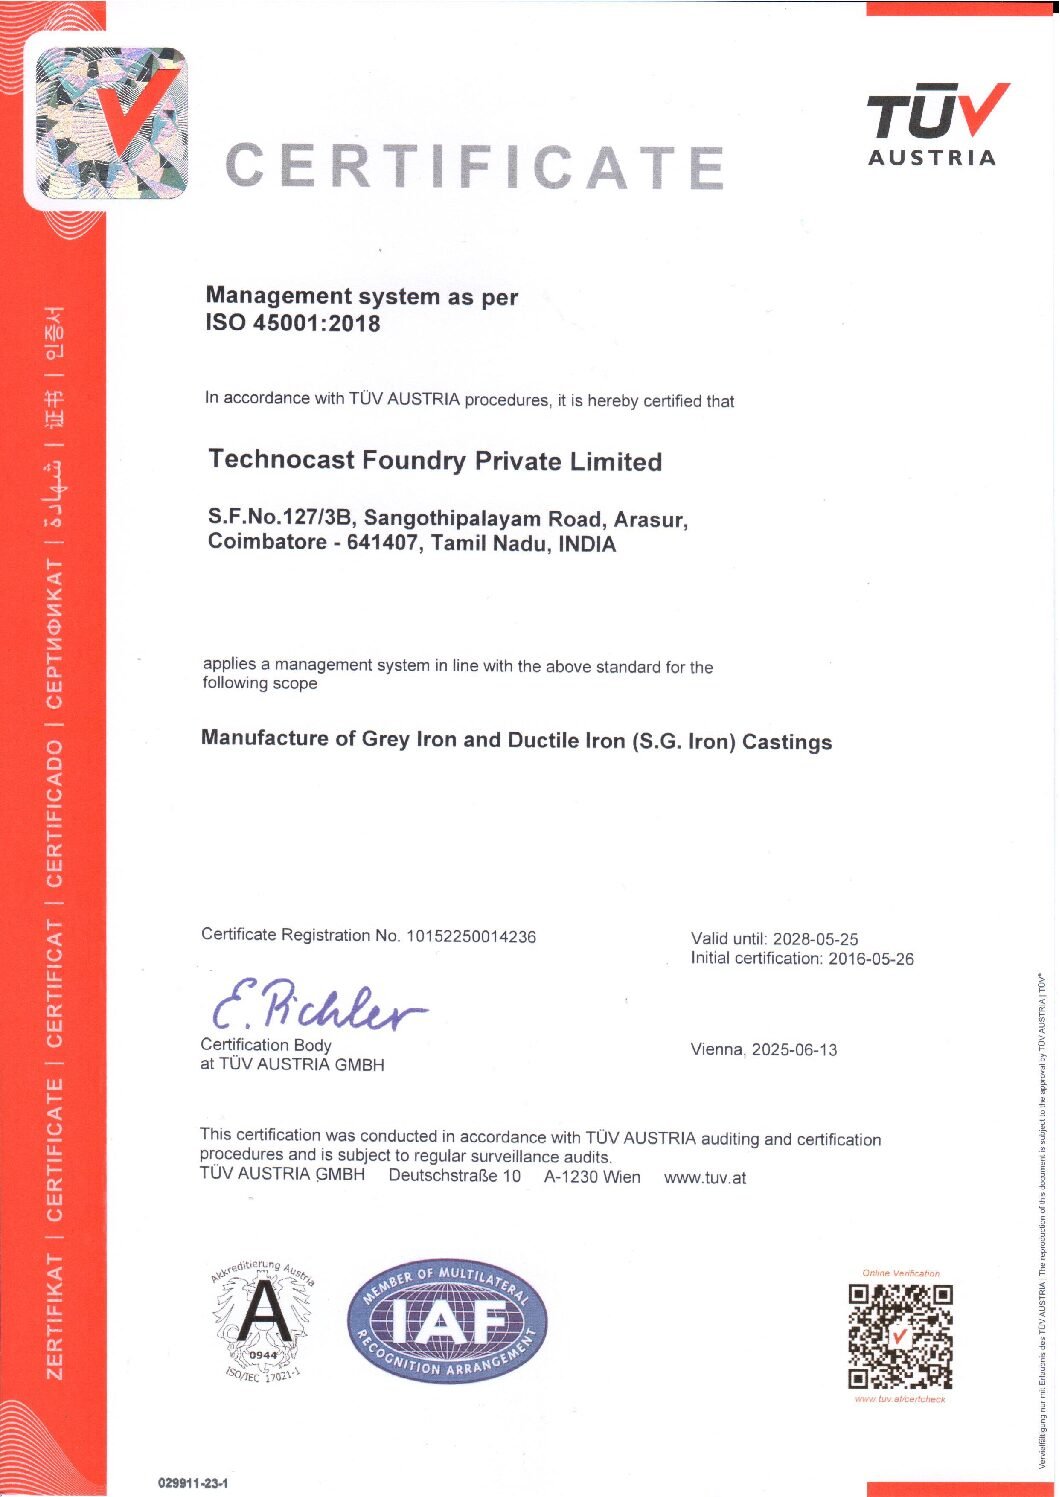
ISO 45001:2018
Occupational health and safety management, across melting, moulding, fettling, heat treatment and machining. TÜV AUSTRIA certificate 10152250014236, certified since May 2016 and valid to 25 May 2028.
Scope Covers
Manufacture of grey iron and ductile (SG) iron castings.
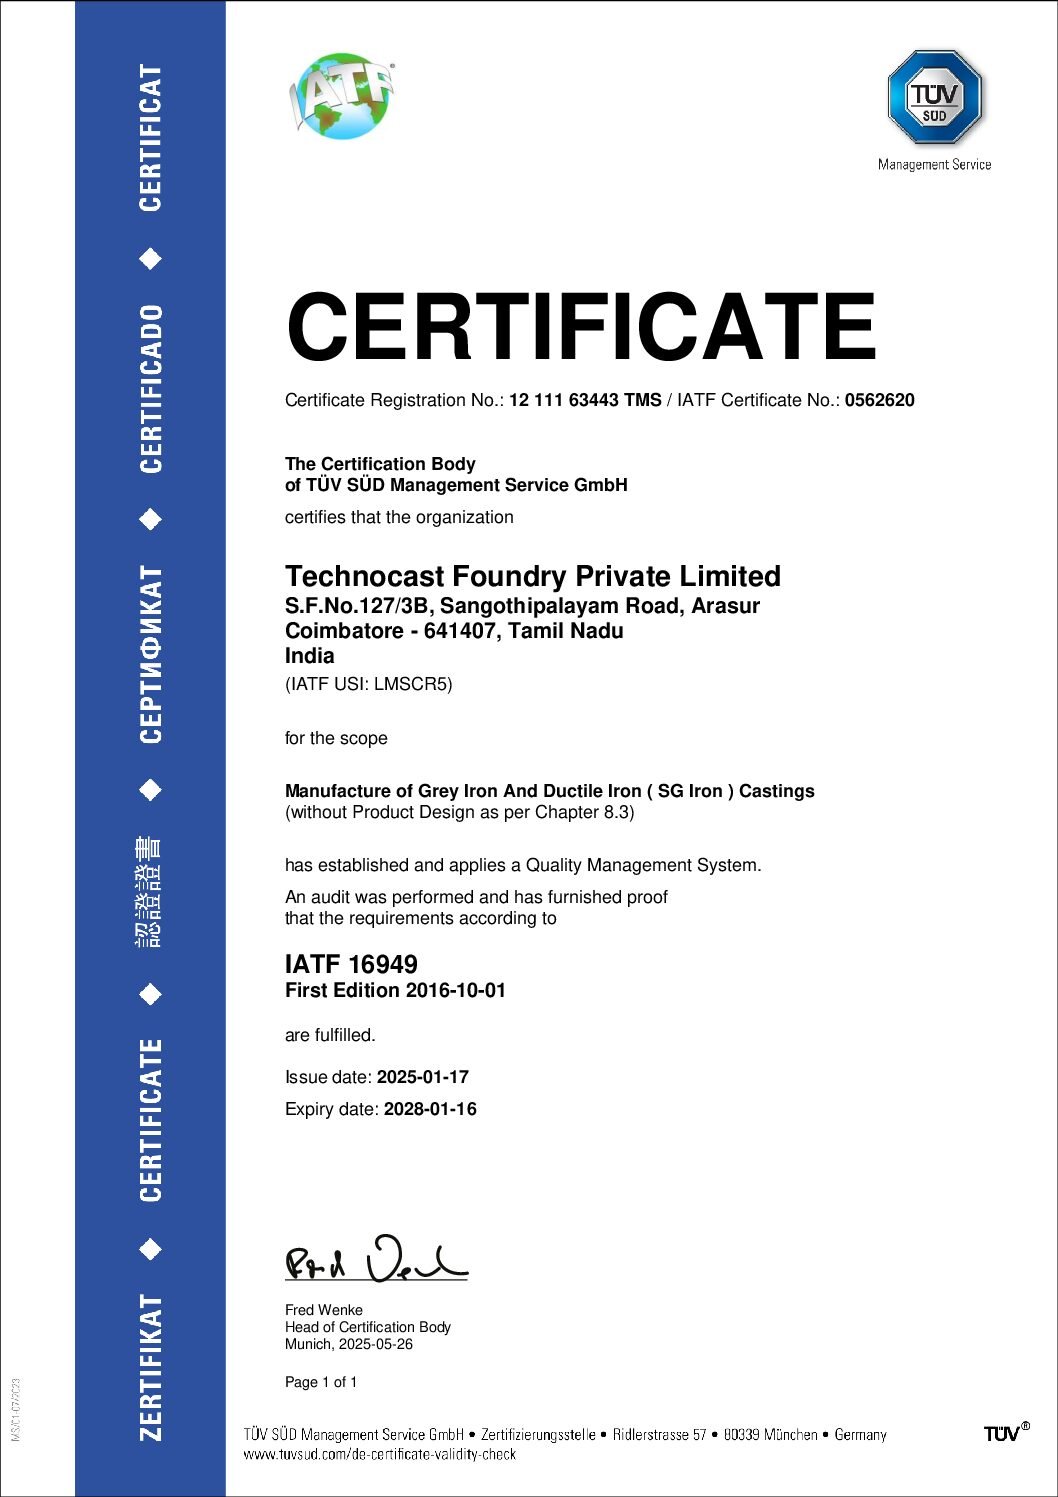
IATF 16949:2016
Automotive quality management, which is what lets us supply OEM and Tier-1 programmes. TÜV SÜD certificate 12 111 63443 TMS, IATF certificate 0562620, valid to 16 January 2028.
Scope Covers
Manufacture of grey iron and ductile (SG) iron castings, without product design under clause 8.3.
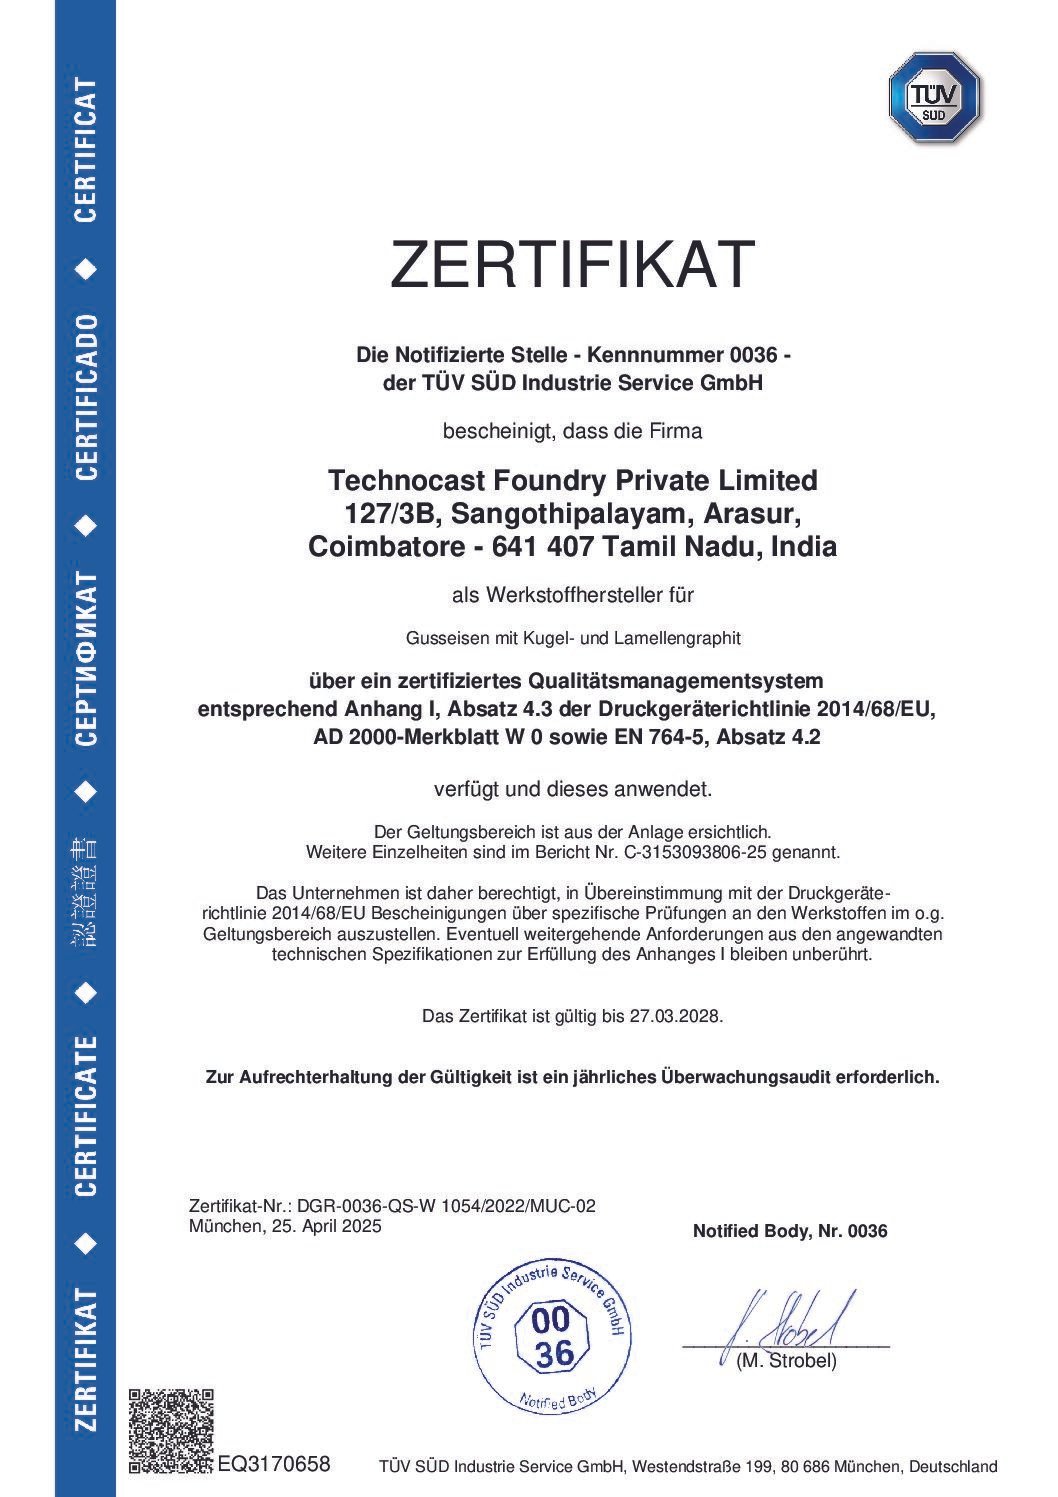
PED 2014/68/EU
Pressure Equipment Directive. Approved as a material manufacturer by TÜV SÜD Industrie Service, Notified Body 0036, under AD 2000-Merkblatt W0 and EN 764-5. Certificate DGR-0036-QS-W 1054/2022/MUC-02, valid to 27 March 2028.
Scope Covers
Ductile and grey cast iron for pressure equipment, with authority to issue specific material inspection certificates.
Control Points
Eight control points sit between raw material and the packing bay. A casting that fails one does not move to the next.
Pig iron, steel scrap, ferroalloys and moulding sand are checked against specification before they are accepted into the plant.
Moulding sand is tested for strength, moisture and permeability on the shop floor. Sand controls surface finish and dimensional accuracy, so it is checked before it is used, not after.
Every heat is analysed on an ARL spectrometer before it is poured. Grey iron, ductile (SG) iron and steel each have their own chemistry window, and the heat is corrected until it sits inside it.
Ductile iron is checked by ultrasonic velocity while the metal is still in the ladle, then confirmed under a microscope with image analyser for graphite shape, size and count.
Tensile strength, elongation and hardness are tested on cast samples from the same heat. Digital micro Vickers is used where a local hardness reading is needed.
Ultrasonic and magnetic particle inspection are carried out in house. Radiographic inspection is arranged through an accredited partner when the drawing calls for it.
Two Brown and Sharpe coordinate measuring machines, contour testing and ring gauge masters confirm the finished part matches the drawing before it leaves the machine shop.
Pressure testing, load testing and dynamic balancing are carried out where the part needs them. The casting is then painted, packed and documented for despatch.
Equipment
All of it is on site at Arasur, Coimbatore. The one exception is radiographic inspection, which is outsourced to an accredited partner.
| Equipment | What it checks |
|---|---|
| ARL spectrometer | Chemical composition of every heat, before pouring |
| Sand testing equipment | Moulding sand strength, moisture and permeability |
| Microscope with image analyser | Graphite shape and count, and matrix structure |
| Ultrasonic velocity instrument | Nodularity check on ductile (SG) iron |
| Tensile and hardness testing machine | Tensile strength, elongation and hardness on cast samples |
| Digital micro Vickers | Local and case hardness readings |
| Brown and Sharpe CMM, 700 x 1,000 x 700 mm | Dimensional inspection with touch probe |
| Brown and Sharpe CMM, 1,500 x 1,200 x 1,000 mm | Dimensional inspection with scanning probe, plus gear profile testing |
| Ultrasonic and magnetic particle equipment | Internal and surface defects, in house |
| Radiographic inspection | Internal soundness where the drawing calls for RT. Outsourced to an accredited partner |
| Contour testing and ring gauge masters | Profile and bore checks against a master |
| Pressure testing rig | Leak testing on pump, valve and hydraulic bodies |
| 2,000 tonne hydraulic press | Load testing to customer specification |
In the Lab
A look at the metallurgical lab, the metrology room and the inspection bay.
Replace with actual plant image
For Your Records
Our current certificates and company brochure, in PDF, for your procurement, vendor approval and audit files.
PDF, 3.4 MB
Company Brochure
42 pages. Plant, moulding routes, machine shop, lab and testing equipment, product range and certifications. Updated August 2026.
PDF, 154 KB
IATF 16949:2016 Certificate
TÜV SÜD Management Service GmbH. Certificate 12 111 63443 TMS, IATF certificate 0562620. Scope: manufacture of grey iron and ductile (SG) iron castings. Valid to 16 January 2028.
PDF, 528 KB
ISO 14001:2015 Certificate
TÜV AUSTRIA. Certificate 10051250014235. Environmental management, certified since May 2016. Valid to 25 May 2028.
PDF, 528 KB
ISO 45001:2018 Certificate
TÜV AUSTRIA. Certificate 10152250014236. Occupational health and safety management, certified since May 2016. Valid to 25 May 2028.
PDF, 872 KB
PED 2014/68/EU Certificate
TÜV SÜD Industrie Service GmbH, Notified Body 0036. Certificate DGR-0036-QS-W 1054/2022/MUC-02. Material manufacturer for ductile and grey cast iron under AD 2000-Merkblatt W0 and EN 764-5. Valid to 27 March 2028.
PDF, 59 KB
Visiting Card
Contact card for T. Kamalakkannan, Managing Director. Direct phone and email, for your vendor and supplier records.
Common Questions
Yes. Technocast holds IATF 16949:2016 alongside ISO 9001:2015, and supplies Tier-1 automotive customers on that basis.
Five: ISO 9001:2015, ISO 14001:2015, ISO 45001:2018, IATF 16949:2016 and PED. All are current and independently audited.
Ultrasonic and magnetic particle inspection are done in house. Radiographic inspection is outsourced to an accredited partner and arranged when the drawing calls for it.
By ultrasonic velocity, then confirmed under a microscope with image analyser for graphite shape, size and count.
Yes. The foundry is PED certified, which is required for castings that go into pressure-bearing equipment sold in the European Union.
The certified scope is the manufacture of grey iron and ductile (SG) iron castings, supplied machined and assembled. We also pour steel, which sits outside that certified scope. Single pieces run from 1 kg to 1,500 kg.
At 127/3B, Sangothipalayam Road, Arasur, Coimbatore, Tamil Nadu 641407, India. The foundry and the machine shop sit on the same 523,200 sq ft site, so buyers in Coimbatore and across Tamil Nadu can audit the whole process in a single visit.
Send a Drawing
Send the drawing with the material grade, the annual quantity and any inspection requirement. You get back a moulding route, a lead time and a price from Arasur, Coimbatore, Tamil Nadu.
Before you go
Our brochure and every current certificate, in PDF, for your vendor file.
Or send us a drawing