Moulding Line · Coimbatore

High Pressure
Moulding Line

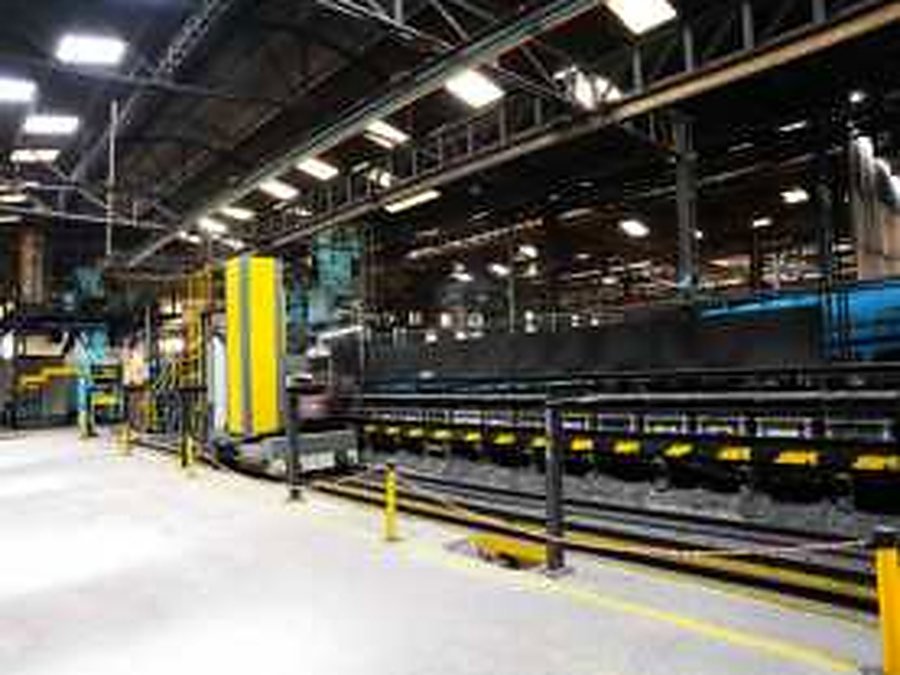
Our DISA MATCH 130 line makes 100 to 120 green sand moulds an hour for iron castings up to 50 kg. It runs at our foundry in Arasur, Coimbatore, Tamil Nadu.

Capability Overview

What Is High Pressure
Moulding Used For?

High pressure moulding is the fastest way to make the same iron casting again and again. Sand is squeezed hard around a matchplate pattern, so every mould has the same density and every casting comes out the same size. It suits parts you order by the thousand.

At Technocast the line is a DISA MATCH 130 with automatic pouring. Mould boxes are 510 x 610 x 400 mm, the line turns out 100 to 120 moulds an hour, and single pieces run up to 50 kg in grey iron and ductile iron.

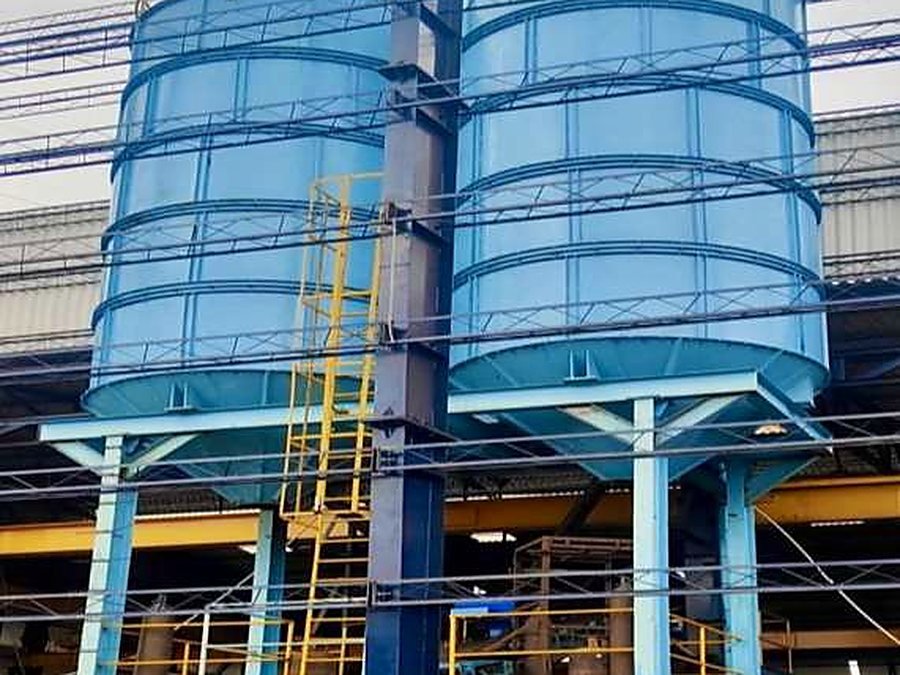
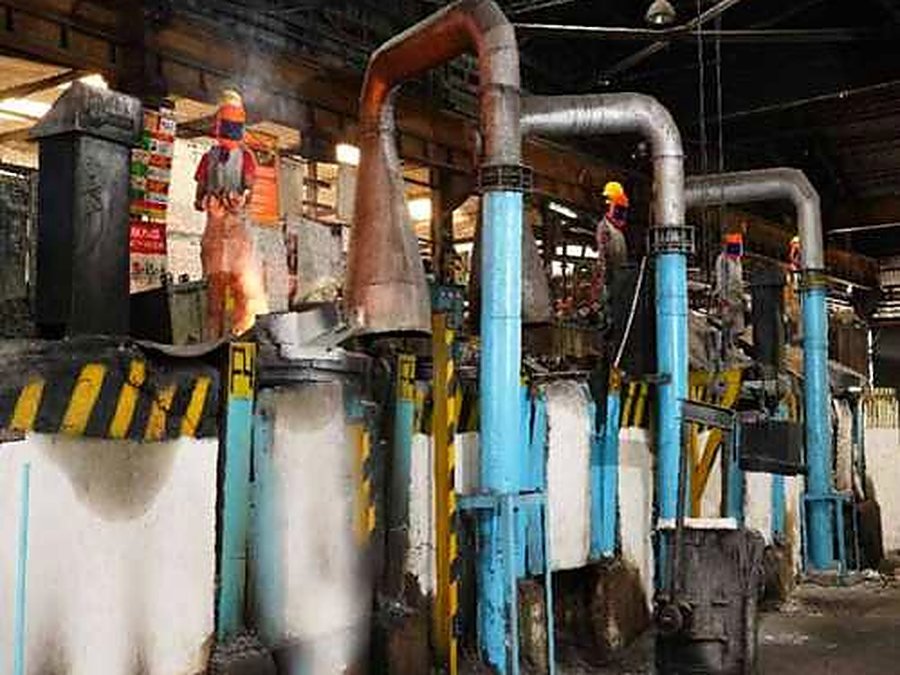
Green sand is prepared by a dedicated sand plant with a SAM 40 continuous mixer and 200 tonnes of storage. Iron comes from four induction furnaces in the same bay. Moulding, melting, machining and testing all sit on one site at Arasur, Coimbatore.

Line Specifications

DISA MATCH 130
Line Specifications

Every figure below is what is installed at the Coimbatore plant. Send a drawing and our engineering team will confirm whether your part suits this line.

Parameter Specification
ProcessGreen sand, high pressure squeeze moulding with horizontal parting
MachineDISA MATCH 130 moulding line with automatic pouring
Mould box size510 × 610 × 400 (200 × 2) mm
Maximum single-piece weightUp to 50 kg
Moulding speed100 to 120 moulds an hour
Metals pouredGrey cast iron and ductile (SG) iron
Sand plantSAM 40 continuous mixer rated 40 tonnes an hour, with 200 tonne storage bunkers
MeltingFour 1-tonne dual-track induction furnaces in the same bay, about 60 tonnes a day
Core makingCold box, shell and CO2 cores from an in-house core shop with shooters from 5 kg to 30 kg
Quality checksSpectrometer reading on every heat, nodularity by ultrasonic velocity, CMM inspection, tensile and hardness testing
Best suited toMedium and high volume repeat parts — brackets, mounts, pulleys, covers and small housings
Plant locationArasur, Coimbatore, Tamil Nadu — foundry, machine shop and testing lab on one site

How It Works

How Does the High Pressure
Moulding Line Run?

Four stages, each with its own check before the casting moves on.

Sand and Pattern Preparation

Matchplate tooling is checked first. Green sand is then mixed and tested for moisture, permeability and strength before it reaches the machine.

Moulding

The DISA MATCH 130 squeezes cope and drag to the same density every cycle. Cores are set where the part needs them, then the mould is closed and clamped.

Melting and Pouring

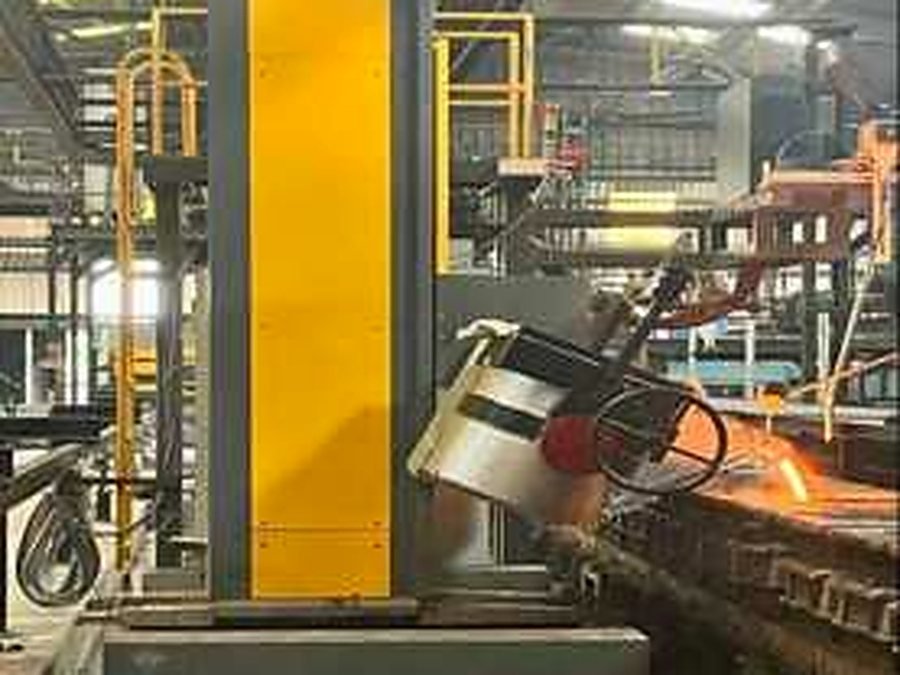
Iron is melted in induction furnaces and checked on the spectrometer before tapping. The automatic pouring unit fills each mould at a controlled temperature.

Cooling, Knockout and Finishing

Moulds cool on the conveyor. Castings are then knocked out, shot blasted and fettled, and checked for dimensions, hardness and structure before dispatch.

Common Questions

High Pressure Moulding
Questions Buyers Ask

What is high pressure moulding?

It is a fast way to make the same iron casting again and again. Green sand is squeezed hard around a matchplate pattern, so every mould has the same density and every casting comes out the same size.

Which high pressure moulding machine does Technocast use?

A DISA MATCH 130 line with automatic pouring, running horizontal parting green sand moulds at our foundry in Arasur, Coimbatore.

What size and weight of casting can the line produce?

The mould box is 510 x 610 x 400 (200 x 2) mm and single pieces run up to 50 kg. Heavier parts move to the ARPA or no bake lines in the same plant.

How many moulds an hour does the line make?

Between 100 and 120 moulds an hour.

Which metals are poured on the high pressure line?

Grey cast iron and ductile (SG) iron. Metal comes from four 1-tonne dual-track induction furnaces in the same bay, about 60 tonnes a day.

What order quantity suits high pressure moulding?

Medium and high volume repeat parts. For one-off, low volume or heavy castings we use ARPA 450, ARPA 1300 or the no bake line instead.

How is the green sand controlled?

A dedicated sand plant prepares it, with a SAM 40 continuous mixer rated 40 tonnes an hour and 200 tonnes of storage. Moisture, permeability and strength are tested before moulding.

What quality checks are done on these castings?

Chemistry is read on the spectrometer at every heat. Nodularity is checked by ultrasonic velocity, dimensions on a CMM, and mechanical properties by tensile and hardness testing.

Can high pressure moulded castings be supplied machined?

Yes. Over 40 CNC machines sit in the same plant, so castings can be shipped fully machined and inspected rather than as-cast.

Where is your high pressure moulding foundry in Tamil Nadu?

At 127/3B, Sangothipalayam Road, Arasur, Coimbatore, Tamil Nadu 641407, India. Plant visits and audits can be arranged through the contact page.
Send Us a Drawing

Need Iron Castings
in Volume?

Tell us the part weight, annual quantity and material. Our team in Coimbatore will confirm whether the high pressure line is the right route.