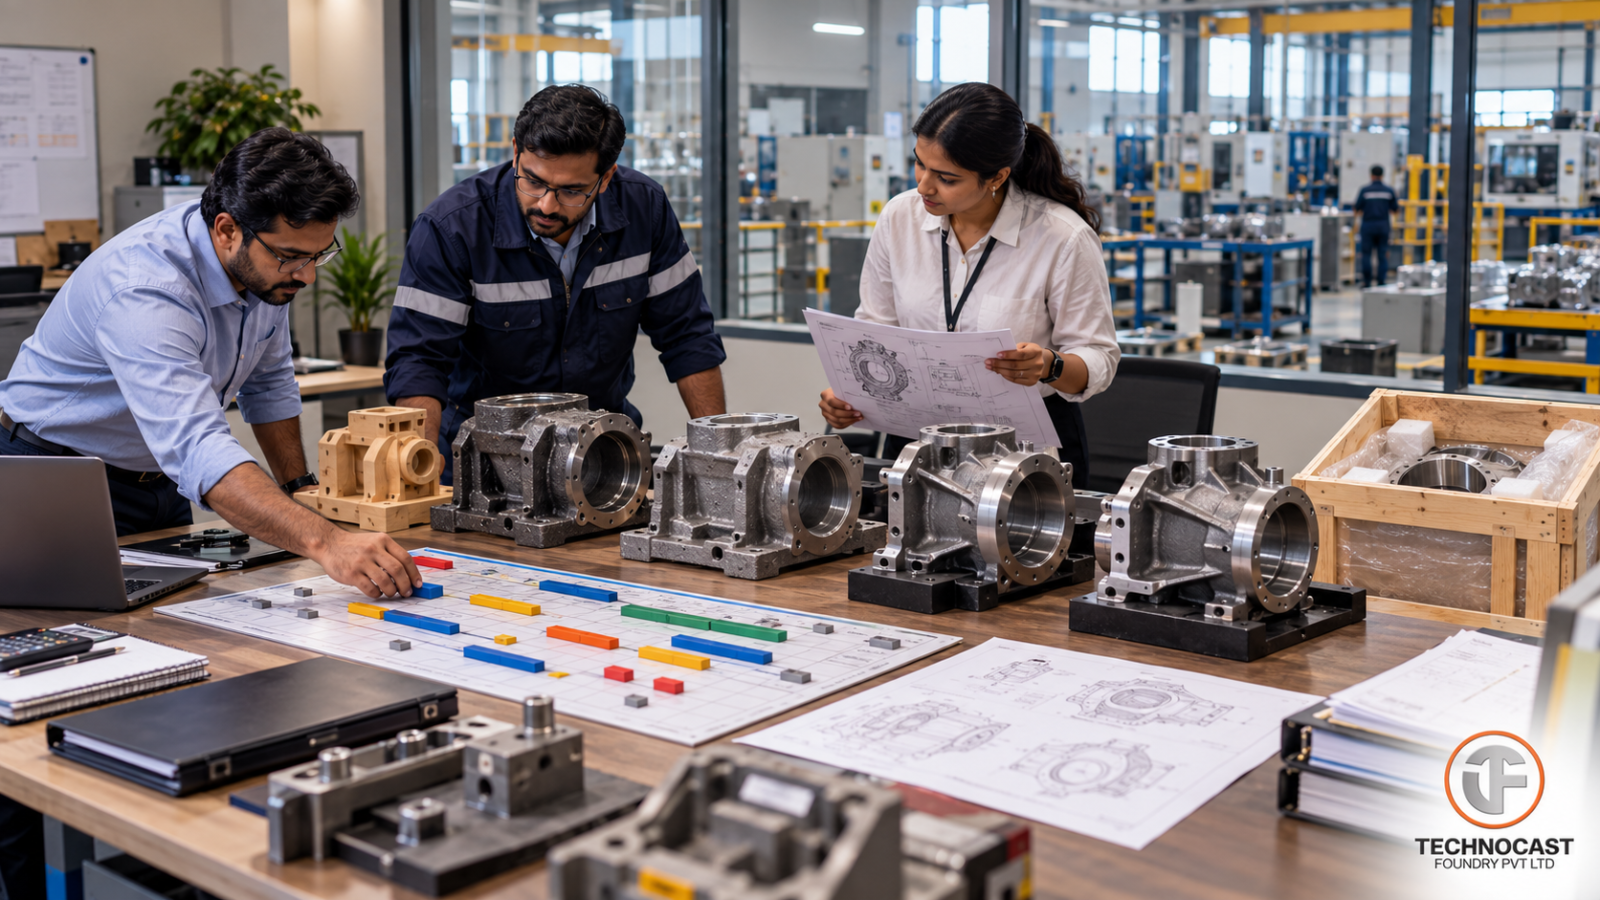
When a casting supplier quotes a lead time, procurement should ask one question immediately:
“Lead time to what?”
Is it:
- Pattern completion?
- First poured casting?
- First machined sample?
- PPAP submission?
- Approved production part?
- Finished component at your receiving dock?
These are very different milestones.
For an OEM procurement team, casting lead time should be measured from released requirements to an approved component in the required delivery condition.
That means the schedule may need to include:
Drawing release → DFM → Tooling → Trial casting → Inspection → Approval → Production casting → Heat treatment → Machining → Finishing → Final inspection → Packing → Transport
The biggest opportunity is often not reducing pouring time.
It is reducing the waiting between operations.
Casting Lead Time Starts Before the Foundry Floor
Many sourcing teams begin measuring lead time from the purchase order or tooling release.
But the actual schedule often starts earlier.
Delays can already be created by:
- Unclear drawings
- Unresolved material specifications
- Missing acceptance criteria
- Late machining input
- Tooling approval delays
- Customer engineering changes
If the foundry cannot confidently release tooling, every downstream milestone moves.
A strong sourcing process therefore starts by asking the supplier for the complete manufacturing and approval schedule, not simply:
“How many weeks for castings?”
Define the Final Delivery Scope First
Before comparing suppliers, define exactly what you expect to receive.
Is the supplier responsible for:
- Raw casting?
- Heat-treated casting?
- Machined casting?
- Finished and inspected component?
- PPAP-approved production part?
- Delivered component at your plant?
Without this definition, two suppliers can quote identical “8-week lead times” while describing completely different delivery conditions.
Procurement comparisons should use the same:
Drawing revision + Quantity + Approval scope + Finished condition + Delivery endpoint
for every supplier.
Build the Lead-Time Map Before Placing the Order
Ask the supplier to divide the program into individual stages.
A useful structure is:
| Stage | What Procurement Should Establish | Release Evidence |
|---|---|---|
| Engineering | Drawing, material and requirements frozen | Approved technical review |
| Tooling | Pattern/core tooling design and manufacture | Tooling inspection/release |
| Trial casting | Sample moulding and pouring | Trial casting available |
| Casting inspection | Dimensions, metallurgy and soundness | Sample inspection accepted |
| Heat treatment | Required treatment and batch scheduling | Accepted treatment records |
| Machining | Fixtures, programs and machine allocation | Machined sample accepted |
| Finishing | Agreed finish and processor | Finish accepted |
| Final inspection | Complete drawing/quality coverage | Release dossier |
| PPAP/FAI | Customer-required approval evidence | Written customer approval |
| Dispatch | Packaging, logistics and documents | Shipping release |
The exact stages will vary by component.
What matters is that every stage has:
an owner + planned date + entry condition + release condition.
Find the Actual Critical Path
Not every operation controls delivery.
A good procurement schedule identifies which operations determine the final completion date.
For example:
Tooling may take four weeks.
But machining fixture manufacture can potentially happen during those same four weeks.
Inspection-program development can also begin before castings arrive.
Packaging design may be prepared before production starts.
If everything is treated sequentially, the program becomes unnecessarily long.
The procurement question should therefore be:
“Which activities are sequential because they technically must be—and which are sequential simply because nobody planned them in parallel?”
Run Engineering Activities in Parallel Where Possible
Consider a new machined housing.
Instead of waiting for the raw casting tool to be complete before discussing machining, the teams can review together:
- Machining stock
- Datums
- Fixture concepts
- Tool access
- Critical dimensions
during casting DFM.
That can allow fixture design and CNC planning to begin while tooling is being manufactured.
The objective is not to start risky work prematurely.
It is to remove avoidable waiting.
Resolve DFM Before Authorising Tooling
One of the most expensive sources of lead-time loss is tooling rework caused by late engineering changes.
Before releasing the pattern, review:
- Draft
- Fillets
- Section transitions
- Core strategy
- Machining allowance
- Datums
- Inspection access
against both the raw-casting and finished-component drawings.
This is particularly important when the foundry and machine shop are separate suppliers.
A casting can be easy to manufacture but difficult to machine.
Conversely, a geometry designed purely around machining can create unnecessary foundry problems.
Freeze the Material Specification Early
Changes such as:
Grey iron → Ductile iron
or:
Carbon steel grade A → Grade B
should not be treated as administrative drawing updates.
Material changes can affect:
- Foundry process
- Heat treatment
- Tooling assumptions
- Inspection
- Qualification requirements
Resolve the material and required properties before production planning wherever possible.
Control Drawing Revisions
A late drawing revision can affect:
- Pattern
- Core box
- CNC fixture
- CNC program
- Gauge
- CMM program
- Inspection plan
- PPAP documents
The supplier should therefore have one clear released drawing revision driving all downstream activities.
When engineering changes occur, the schedule should show:
What changed?
Which processes are affected?
Who approves the revised timing?
Tooling Lead Time Needs Its Own Milestones
Do not treat tooling as one black-box activity ending with:
“Pattern complete.”
Break it into stages such as:
- Tooling concept approval
- Pattern/core-box manufacture
- Tooling inspection
- Trial assembly
- First mould
- First casting
- Dimensional review
- Tool correction if required
This makes tooling delays visible earlier.
Tooling and Machining Fixtures Should Be Coordinated
A common problem is:
Casting tooling is ready, but machining fixture is not.
The first casting then waits.
If the finished component requires machining, the tooling schedule should include both:
Foundry tooling
and:
Machining fixtures/program preparation.
The program is only as fast as the slowest required production asset.
Use Rapid Tooling Carefully
Printed patterns, cores and other rapid-development methods can shorten early iterations for suitable applications.
But procurement should separate:
Prototype acceleration
from:
Production process readiness.
A rapidly produced prototype does not automatically prove that the final serial-production tooling and process are ready.
Ask the supplier to explain:
- What rapid method is being used
- Which qualification question it answers
- Whether the production process will be identical
- What additional validation remains
Digital Engineering Can Save Time Before Tooling
Simulation and digital DFM can reduce trial-and-error when they resolve engineering decisions before physical tooling.
A useful digital review should answer questions such as:
- Can the section fill?
- Where are heavy thermal regions?
- Where might shrinkage occur?
- Is feeding adequate?
- Is the proposed change better?
The value is not simply:
“Simulation completed.”
It is:
“A production decision was made earlier because engineering evidence was available.”
Map External Handoffs
If operations occur at different suppliers, each transfer needs its own schedule.
For example:
Foundry → Heat treatment
may involve:
- Job completion
- Packing
- Transport booking
- Collection
- Transit
- Goods receipt
- Queue
- Incoming inspection
A commercial quote may show only:
“Heat treatment: 3 days.”
But the actual elapsed time could be much longer because the part waits before and after those three processing days.
Procurement should therefore measure:
Elapsed lead time
not only:
Process cycle time.
Ask What Actually Stays In-House
A supplier may describe itself as an integrated manufacturer while outsourcing some operations.
That is not necessarily a problem.
But the schedule should make external steps visible.
For the proposed component, ask whether these operations are internal or external:
- Pattern/tooling
- Casting
- Heat treatment
- CNC machining
- NDT
- Surface finishing
- Special testing
- Packaging
Then ask:
What happens when an outsourced processor misses its slot?
Integration Should Be Evaluated Against the Real Route
Do not assume that one-site production automatically provides a shorter lead time.
A fully integrated supplier can still have internal bottlenecks.
Evaluate:
- Available moulding capacity
- Furnace capacity
- Heat-treatment slots
- Machining capacity
- Inspection capacity
for your actual component.
The important comparison is:
Supplier A’s complete route vs Supplier B’s complete route.
Do Not Confuse Moulding Speed With Delivery Speed
An automated moulding line may produce moulds very quickly.
That does not necessarily mean your finished component has a short lead time.
The critical path may instead be:
- Core availability
- Heat treatment
- CNC machining
- CMM inspection
- Customer approval
When comparing DISA-type high-pressure moulding with no-bake production, procurement should focus first on process fit.
DISA High-Pressure Moulding
For suitable repetitive components, ask whether:
- Component envelope fits the line
- Tooling is suitable
- Core setting is practical
- Forecast volume supports the route
- Capacity is available
No-Bake Moulding
For larger or more complex parts, ask whether no-bake better supports:
- Component size
- Core package
- Geometry
- Production mix
The faster moulding process is not automatically the faster sourcing solution.
Capacity Must Be Checked at the Bottleneck
Foundry capacity stated in tonnes per month is useful background information.
It does not prove that your component has a production slot.
A supplier might have plenty of melting capacity but limited:
- Moulding availability
- Core capacity
- Heat-treatment capacity
- CNC machine hours
- Inspection resources
Ask:
“Which work centre is the constraint for my part?”
Then ask for available capacity at that work centre.
Forecasts Matter
Production planning becomes more reliable when suppliers have usable demand forecasts.
Procurement should clarify:
- Annual volume
- Monthly demand
- Peak demand
- Ramp-up
- Expected batch sizes
Then understand how the supplier reserves capacity.
An annual forecast of 12,000 pieces does not automatically mean:
1,000 pieces every month.
The actual production profile matters.
Schedule PPAP Before Tooling Release
PPAP should not appear at the end of the project as:
“Now prepare the documents.”
For programs requiring PPAP, the submission plan should be defined early.
Agree:
- Submission level/scope required by the customer
- Sample quantity
- Production conditions
- Dimensional layout
- Material testing
- MSA
- Capability studies where required
- Control Plan
- PFMEA
- Approval authority
This allows documentation to develop in parallel with tooling and process development.
Treat First Article Approval as a Workstream
First Article Inspection should also be scheduled.
Define:
Which component will be inspected?
Which drawing revision?
Which characteristics?
Which material/test evidence?
Who reviews it?
How quickly?
Otherwise the supplier may complete samples on Friday and then wait two weeks for customer engineering approval.
That waiting time is part of the program lead time.
Use Explicit Approval Gates
A useful qualification schedule can contain five major gates.
Gate 1 — Requirements Agreed
Confirm:
- Drawing
- Material
- Specifications
- Customer requirements
Gate 2 — Process Ready
Confirm:
- Tooling
- Fixtures
- Manufacturing route
- Inspection methods
Gate 3 — Samples Complete
Required production, machining and testing have been completed.
Gate 4 — Submission Complete
All required reports and evidence have been checked.
Gate 5 — Production Released
Customer approval/disposition has been received.
Production shipment should not be assumed before the required approval gate.
Include Customer Review Time
Lead time is not controlled only by the supplier.
OEM approval can become part of the critical path.
Procurement should therefore define:
- Customer reviewer
- Review window
- Escalation route
- Deviation process
- Resubmission timeline
This prevents a technically completed sample from sitting in an inbox without a decision.
Prepare Documentation While Tooling Is Being Manufactured
Several quality activities can begin before the first component exists.
Examples include:
- Inspection-plan preparation
- Ballooned drawing
- Report templates
- CMM program planning
- PFMEA
- Control Plan
- Traceability format
This reduces administrative waiting after the samples are produced.
Repeat-Order Lead Time Is Different From New-Program Lead Time
Do not compare a repeat-order lead time with a new-tool launch.
A routine repeat order may assume:
- Tooling already exists
- Tooling is serviceable
- Drawing is unchanged
- Process is approved
- Fixtures exist
- Customer approval is complete
Those assumptions should be stated explicitly.
Check Tooling Condition Before Committing the Date
Retained tooling may need:
- Inspection
- Repair
- Maintenance
- Replacement
before production.
A supplier should not promise the previous repeat-order lead time until tooling condition is known.
Revised Components Are Not Routine Reorders
A part may have the same part number family but require:
- New tooling
- Modified core box
- Fixture changes
- CNC program changes
- Requalification
because the drawing changed.
Treat transferred or modified programs separately from routine repeat business.
Progress Reporting Should Follow Milestones
“Production is in progress” is not an adequate status update.
A useful progress report should state:
- Completed milestone
- Current operation
- Next gate
- Outstanding customer decision
- Risk
- Current dispatch forecast
When the forecast changes, require the reason.
This helps procurement identify problems while there is still time to recover.
Escalation Should Be Defined Before a Delay
Before placing the order, agree:
- Primary project contact
- Technical contact
- Escalation contact
- Recovery-plan format
Do not create an escalation process after the program is already late.
What a Recovery Plan Should Explain
When a milestone slips, the supplier should explain:
What happened?
Which downstream milestones are affected?
What can run in parallel?
What resources are being added or reprioritised?
What is the revised dispatch date?
The objective should be a realistic recovery plan, not another optimistic date.
How Technocast Fits Into a Lead-Time Review
For suitable programs, Technocast’s integrated ferrous manufacturing capabilities can allow several parts of the manufacturing route to be coordinated under one supplier relationship.
Relevant established capabilities include:
- Ferrous casting
- Multiple moulding routes
- Heat treatment
- CNC machining
- Spectrometry
- CMM dimensional inspection
- Ultrasonic testing where applicable
For example, heat chemistry verification and final dimensional inspection can be built into the same overall production plan rather than treated as unrelated activities.
However, the correct lead time should still be developed for the specific component.
It should consider:
- Tooling status
- Selected moulding route
- Material
- Casting weight
- Heat treatment
- Machining content
- Inspection
- External processes where required
- Customer approval
Do not convert Technocast’s installed equipment or overall capacity into a universal lead-time promise.
Casting Lead-Time RFQ Checklist
When requesting quotation and schedule, provide:
Drawing and Revision
Use the released revision.
Material Grade
Avoid unresolved material alternatives.
Casting Weight
Provide expected weight where available.
Annual Volume
Include peak requirements.
Final Supply Scope
State clearly:
- Raw casting
- Heat-treated
- Machined
- Finished
- Inspected
Tooling
Clarify:
- New tooling
- Customer-owned tooling
- Existing tooling
- Transfer tooling
Quality Approval
Define:
- FAI
- PPAP where applicable
- Sample quantities
- Documentation requirements
External Operations
Require the supplier to identify them.
Delivery Endpoint
Specify whether lead time ends at:
- Supplier dispatch
- Port
- Customer warehouse
- Production plant
Five Questions Procurement Should Ask Before Accepting a Lead Time
1. What is the critical path?
The supplier should be able to identify it.
2. Which operations will run in parallel?
This shows whether the schedule has been engineered or merely added together.
3. Where are the external handoffs?
Hidden third-party processes can become major schedule risks.
4. What capacity has actually been reserved?
Installed capacity is not the same as available capacity.
5. What approval is required before production shipment?
Customer review time needs to be part of the schedule.
Conclusion
Reducing casting lead time does not mean asking the foundry to pour faster.
The largest delays often occur before, between and after manufacturing operations.
A robust sourcing schedule connects:
Engineering release → Tooling → Casting → Heat treatment → Machining → Inspection → Approval → Logistics
with a clear owner and release condition at every stage.
Procurement should therefore reject vague promises such as:
“Delivery in six weeks.”
Instead ask:
What happens during those six weeks?
Which operation controls completion?
What happens in parallel?
Which external processors are involved?
When does customer approval occur?
What evidence releases the next stage?
The best supplier is not necessarily the one quoting the shortest lead time.
It is the supplier whose schedule is technically realistic, capacity-backed and transparent enough to manage before a delay occurs.
Build a More Reliable Casting Schedule
For a new or re-sourced casting, send Technocast:
- Drawing
- Material grade
- Single-piece weight
- Annual volume
- Machining scope
- Heat-treatment requirement
- Inspection requirement
- PPAP/FAI requirements
- Required delivery condition
The manufacturing route can then be reviewed against the appropriate moulding process, downstream operations and approval requirements before the final schedule is committed.
Frequently Asked Questions
What usually controls casting lead time?
It depends on the program. Tooling, customer approval, heat treatment, machining, cores or inspection can become the critical path—not necessarily moulding or pouring.
How can tooling lead time be reduced?
Complete DFM early, freeze requirements, coordinate casting and machining tooling, and use rapid tooling methods where technically appropriate.
Does an automated moulding line automatically mean shorter lead time?
No. A fast moulding cycle does not help if cores, machining, heat treatment or customer approval are the bottlenecks.
How should procurement compare two suppliers’ lead times?
Give both suppliers the same drawing revision, quantity, approval scope, finished condition and delivery endpoint, then compare the complete stage-by-stage schedules.
Should PPAP time be included in casting lead time?
If production shipment depends on PPAP approval, yes. Sample production, document preparation, customer review and any resubmission should be included in the program schedule.
Why do external suppliers increase lead time?
External processes can add transport, goods receipt, queues, inspection and scheduling dependencies around the actual processing time.
Is repeat-order lead time shorter than first-order lead time?
Usually, provided tooling remains serviceable, drawings are unchanged, processes remain approved and capacity is available.
What should a supplier progress report contain?
It should identify completed milestones, current operation, next release gate, outstanding decisions, risks and the current forecast dispatch date.